FAMILY 03 · SIBLING COMPONENT
3.2 Overmolded Lead Screws & Shafts
Wear-resistant, self-lubricating engineering plastics molded directly onto stainless steel lead screws, motor rotor shafts, or brass guide cores.
Explore Overmolded Lead Screws →Home › Products › 03 Insert & Stator Overmolding › Stator Overmolding
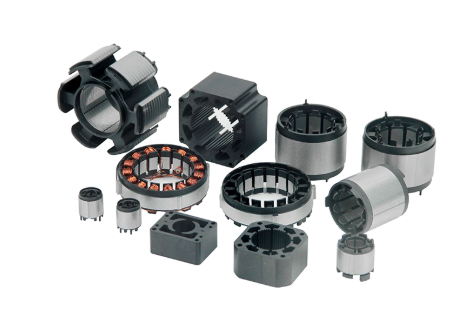
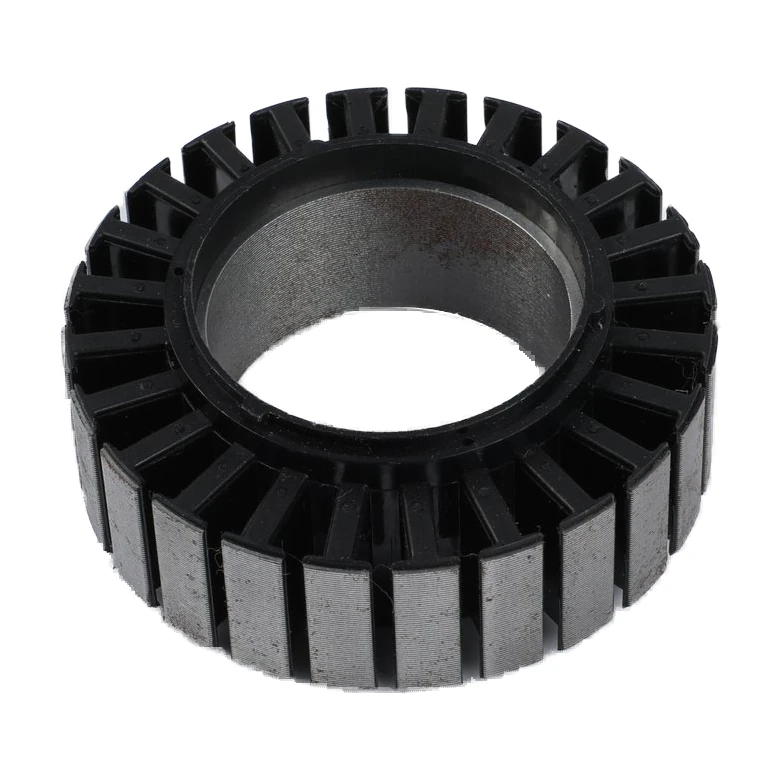
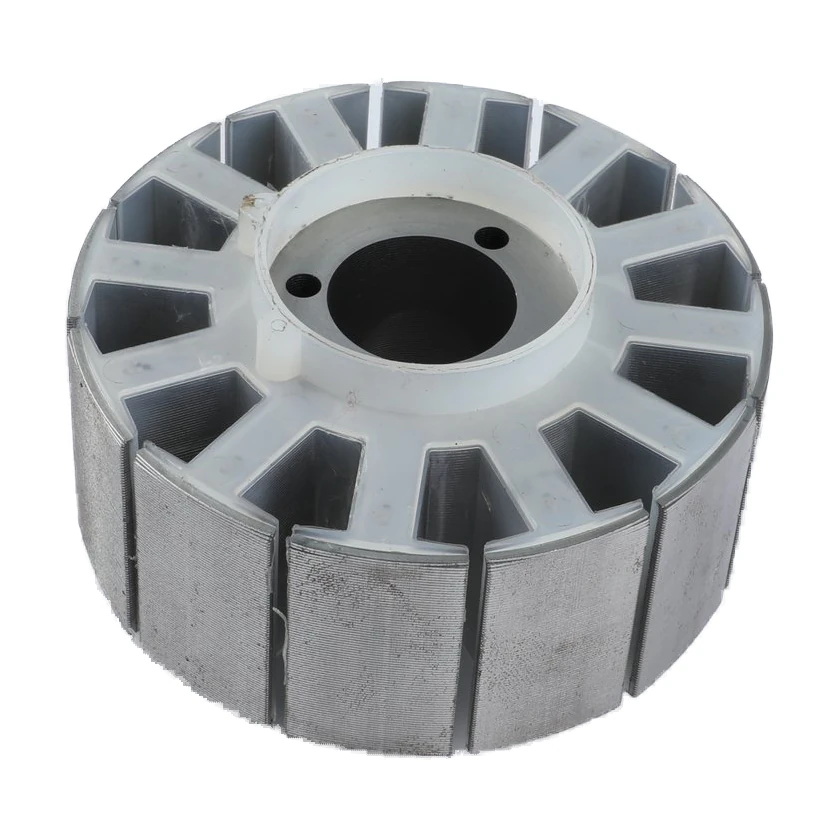
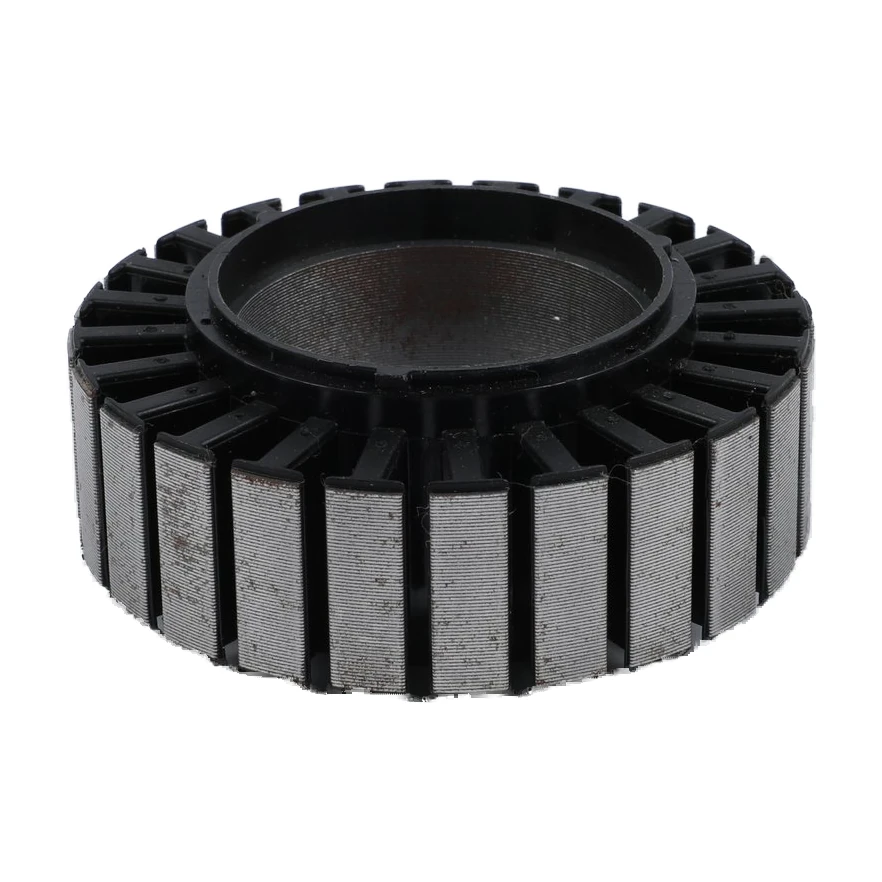
Direct high-adhesion polymer encapsulation molded onto customer-supplied or in-house sourced laminated silicon-steel stator cores. Engineered with DuPont/BASF modified PPS, PA46, and PA66+GF to replace multi-piece assembled bobbins—eliminating air gaps, preventing thermal delamination, and improving heat dissipation.
✓ Delamination-Free Metal-Plastic Bonding
✓ Zero Flash on Stator Bore & Teeth
✓ 100% High-Pot & Coaxiality Verified
PRECISION TOLERANCE
CORE POLYMERS
SAFETY & COMPLIANCE
TOOLING & LEAD TIME
WHY ENGINEERS CHOOSE RUNHENG STATOR OVERMOLDING
Controlled pre-heating of silicon-steel stator stacks paired with low-shrinkage modified PPS/PA66+GF prevents weld-line cracking or plastic-to-metal delamination across -40°C to 220°C+ thermal shocks.
Micron-level Charmilles Wire EDM mold shutoffs seal tightly against stator lamination stack tolerances, keeping the inner rotor bore and outer mating diameter 100% free of plastic flash.
Direct thin-wall slot encapsulation (down to 0.12mm–0.3mm) eliminates the air gap between plastic and steel, lowering thermal resistance and increasing copper winding space.
Dedicated vertical rotary-table injection presses protect delicate silicon-steel laminations from clamping deformation while maintaining ±0.02mm coaxiality.
TECHNICAL SPECIFICATIONS
Available Overmolding Resins
High-Flow Modified PPS, PA46, PA66+GF (15%–35%), LCP, PBT+GF (DuPont / BASF Partners)
Flame Retardancy & Tracking
UL94 V-0 Certified; CTI ≥ 600V High-Voltage Tracking Resistance
Minimum Slot Wall Thickness
Down to 0.12mm–0.35mm Uniform Slot Insulation (±0.02mm Tolerance)
Thermal Endurance
180°C to 220°C+ Continuous Operating Temperature
Metal Core Supply Mode
Overmolding on Customer-Supplied Unwound Cores OR Turnkey Core + Overmolding
Mold Clamping Protection
Spring-Loaded Stack Height Compensation & Precision Center-Bore Arbors
Quality & Defect Control
≤ 50 PPM; 100% Inner-Bore Go/No-Go Gauging & High-Pot Breakdown Testing
Certifications
ISO 9001:2015, ISO 14001:2015, UL Process Certified, RoHS & REACH
STANDARD & CUSTOM CONFIGURATIONS
Direct insulating coating inside winding slots and on both stack ends, replacing separate top/bottom bobbins and slot paper.
Inquire Unwound Stators → Overmolded multi-slot outer-rotor cores with integrated central bearing boss and mounting flange.
Request Custom Quote → Complete polymer overmolding over stator assemblies for submersible pumps, marine thrusters, and outdoor actuators.
Discuss Waterproof Molding →HOW WE GUARANTEE CONSISTENCY
Incoming silicon-steel cores are inspected for stack height tolerance, cleaned of stamping oil, and pre-heated to prevent premature melt freeze-off.
Symmetric pin-point gating ensures even melt pressure around every stator tooth without bending thin laminations.
Every overmolded stator undergoes inner-bore concentricity gauging and 1.5kV–3kV AC dielectric withstand voltage verification.
03 / INSERT MOLDING & STATOR OVERMOLDING FAMILY
FAMILY 03 · SIBLING COMPONENT
Wear-resistant, self-lubricating engineering plastics molded directly onto stainless steel lead screws, motor rotor shafts, or brass guide cores.
Explore Overmolded Lead Screws →FAMILY 03 · SIBLING COMPONENT
High-strength metal-plastic composite components combining splined brass or steel bushings with lightweight, vibration-damping engineering plastics.
Explore Bushings & Limiters →FAMILY 03 · SIBLING COMPONENT
Precision internal threads and splines formed directly inside the injection mold for hollow-core motor shafts.
Explore Hollow Threaded Shafts →DIRECT ENGINEERING SUPPORT
Upload or email your 2D/3D component drawing (STEP, IGES, DWG, PDF) or share your component geometry. Free standard stock samples are available (freight collect), and custom DFM reviews are returned within 24 business hours.
✓ Free Standard Stock Samples (Freight Collect)
✓ 24-Hour Engineering DFM & Quote Response
✓ 100% NDA Confidentiality Protection
Fill out the project specs below or attach your CAD files. Our engineering team responds within 24 business hours.